

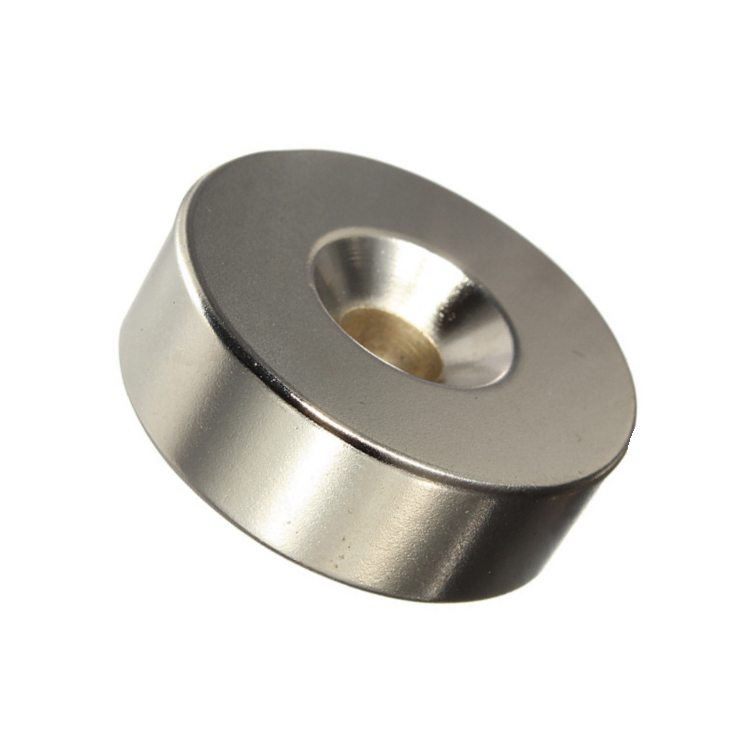
Bonding permanent magnets to metal components is a common assembly method in electric motors, sensors, magnetic couplings, automation equipment, and other industrial applications. However, choosing an adhesive for magnets involves more than finding a glue that can hold two surfaces together. The magnet coating, metal substrate, joint geometry, operating temperature, and mechanical loads all affect long-term bonding reliability.
A suitable magnet bonding adhesive must provide adequate adhesion to both surfaces while maintaining its performance under actual service conditions. Poor surface preparation, an unsuitable adhesive, or an improperly designed joint can cause magnets to shift, detach, or fail during operation.
This guide explains how to select an adhesive for magnets, prepare bonding surfaces, design reliable adhesive joints, and improve the consistency of magnetic assembly bonding in industrial applications.
Why Is Magnet-to-Metal Bonding Challenging?
Permanent magnets and metal components have different physical and surface characteristics. These differences can make adhesive bonding more complicated than joining two ordinary metal parts.
For example, sintered neodymium magnets are relatively brittle. Excessive mechanical pressure or impact during assembly can cause chipping or cracking. Their surfaces are also commonly protected by coatings such as nickel-copper-nickel, zinc, or epoxy. The adhesive must therefore bond reliably to the actual coating rather than being selected only for its compatibility with the underlying magnet material.
The metal substrate introduces another variable. Steel, aluminum, stainless steel, and coated metal surfaces can have different surface conditions and preparation requirements. Oil, dust, oxidation, paint, and machining residues may reduce adhesion.
Industrial assemblies also experience operating loads that can weaken a poorly designed joint, including:
- Vibration and repeated mechanical movement
- Centrifugal forces in rotating assemblies
- Thermal expansion and contraction
- Impact and shock loading
- Moisture, oils, coolants, and cleaning chemicals
For these reasons, bonding magnets to metal should be treated as an engineering joint-design task rather than a simple adhesive application.
How to Choose the Right Magnet Bonding Adhesive
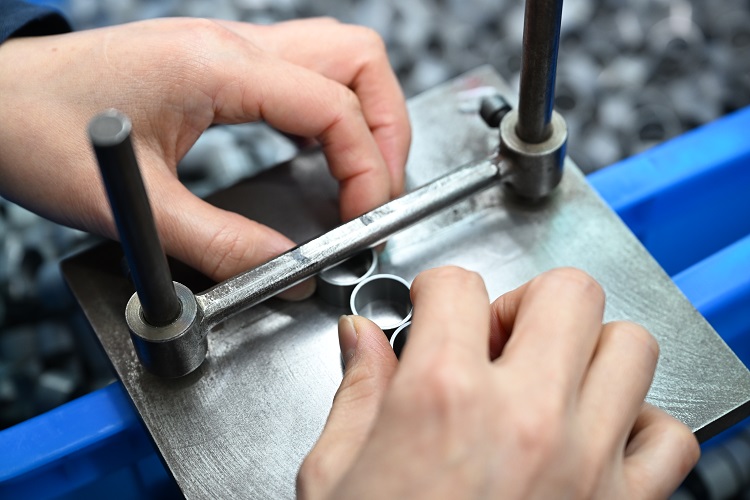
There is no universal adhesive suitable for every magnet assembly. The right choice depends on the magnet coating, metal substrate, bondline gap, required strength, production process, and service environment.
The following adhesive families are commonly considered for industrial magnet bonding.
Epoxy Adhesives
Two-part epoxy adhesives are widely used for structural bonding because many formulations provide high strength, good environmental resistance, and useful gap-filling capability.
They can be suitable for bonding permanent magnets to steel, aluminum, and other properly prepared metal substrates. Epoxy is often considered when an assembly needs reliable retention under vibration, mechanical loading, or temperature variation.
However, epoxy formulations differ considerably. Their working time, curing schedule, flexibility, impact resistance, and maximum service temperature depend on the specific product.
Before selecting an epoxy adhesive, check:
- Compatibility with the magnet’s surface coating
- Adhesion to the selected metal substrate
- Recommended bondline thickness
- Mixing ratio and working time
- Fixture time and full curing conditions
- Temperature and chemical resistance after curing
Epoxy is a useful starting point for many structural magnet-bonding applications, but the actual formulation must be qualified for the assembly.
Structural Acrylic Adhesives
Structural acrylic adhesives are another option for magnet adhesive selection, particularly in production environments where shorter fixture times are important.
Many acrylic systems offer fast strength development and can bond a range of metal surfaces. Some formulations may tolerate certain levels of surface contamination better than conventional epoxy systems, although proper surface preparation remains important for reliable bonding. This does not mean that cleaning and surface preparation can be ignored.
Acrylic adhesives may be considered for:
- High-volume magnet assembly
- Production lines requiring shorter fixture times
- Metal-to-magnet joints with suitable surface compatibility
- Assemblies where the adhesive supplier confirms the required environmental performance
The main considerations include odor, working time, mixing or activation requirements, substrate compatibility, and the adhesive’s long-term performance under the expected loads.
Cyanoacrylate and Flexible Adhesives
Cyanoacrylate adhesives, often called instant adhesives, cure quickly and can be useful for small magnets with close-fitting bonding surfaces and relatively light service loads.
However, many cyanoacrylate formulations form comparatively rigid bondlines. They may be less suitable for joints exposed to repeated impact, significant peel stress, or large gaps.
Flexible adhesives, such as certain polyurethane or silicone systems, may be considered when vibration isolation, flexibility, or differences in thermal expansion are important. Their strength, temperature resistance, and chemical compatibility must still be checked against the application requirements.
Epoxy vs. Acrylic Adhesive for Magnet Bonding
| Selection factor | Epoxy adhesive | Structural acrylic adhesive |
|---|---|---|
| Structural bonding | Many formulations provide high strength | Many formulations provide high strength |
| Fixture speed | Often slower | Often faster |
| Surface preparation | Usually requires thorough preparation | Some formulations tolerate certain surface conditions better |
| Gap filling | Depends on formulation; many options offer useful gap filling | Depends on formulation and joint design |
| Impact and vibration | Depends on toughness and formulation | Depends on formulation |
| Production suitability | Suitable when the curing cycle fits the process | Often useful for faster production cycles |
This comparison is a general selection guide, not a substitute for product-specific technical data. Always compare the actual adhesive specifications and test the complete magnet-to-metal joint.
Surface Preparation Before Bonding Magnets to Metal
Surface preparation is one of the most important factors in adhesive bonding reliability. Even a high-performance adhesive can fail when it is applied to contaminated, incompatible, or poorly prepared surfaces.
Identify the Magnet Coating
Before choosing an adhesive, identify the magnet’s external surface.
Common neodymium magnet finishes include:
- Nickel-copper-nickel plating
- Zinc coating
- Epoxy coating
- Other specified protective finishes
The adhesive normally bonds to this external finish. Therefore, the coating’s adhesion to the magnet and its compatibility with the adhesive are both important.
For example, a smooth plated surface may require a different preparation method from an epoxy-coated surface. Aggressive sanding can damage a protective coating and expose corrosion-sensitive NdFeB material.
Do not assume that every coating should be abraded. Follow the magnet supplier’s and adhesive manufacturer’s preparation recommendations, then validate the process on representative parts.
Clean and Prepare Both Bonding Surfaces
Both the magnet and the metal substrate need appropriate preparation.
A typical preparation sequence may include:
- Inspect both surfaces for oil, dust, corrosion, paint defects, or other contamination.
- Remove compatible surface contaminants using a cleaning method approved for the materials.
- Apply controlled abrasion only when recommended for the specific coating and substrate.
- Remove loose particles and cleaning residues.
- Allow the surfaces to dry completely.
- Apply the adhesive within the qualified process window.
Solvent compatibility is important. A cleaning agent that works on steel may damage a coating, plastic component, or other assembly material. Always confirm the approved cleaning method before production.
How to Design a Reliable Magnet Adhesive Joint
Choosing an appropriate adhesive is only part of the process. The joint geometry and load direction also determine whether the magnet remains securely attached.
Bond Area and Bondline Thickness
The available bonding area should be sufficient for the expected loads and the adhesive’s validated performance.
A larger bonding area can help distribute load, but simply increasing the amount of adhesive does not guarantee a stronger joint. Excessive adhesive can create alignment problems, inconsistent bondline thickness, or unwanted material squeeze-out.
Bondline thickness should follow the adhesive manufacturer’s recommended range. Spacers, controlled recesses, dispensing equipment, or other process controls can help maintain a consistent gap.
For magnetic assemblies, adhesive thickness can also affect the magnetic gap and the final position of the magnet. This is particularly important in compact magnetic circuits and precision motor assemblies.
Shear, Peel, and Tensile Loads
Adhesive joints generally perform differently depending on the direction in which the load is applied.
- Shear loading: The joined surfaces slide relative to each other. Many structural adhesives perform well in properly designed shear joints.
- Peel loading: A force lifts one edge of the bonded component away from the substrate. This can concentrate stress near the joint edge.
- Tensile loading: The components are pulled directly apart across the bondline.
- Cleavage loading: A separating force acts at one end of a joint and creates concentrated stress.
Where possible, design magnet assemblies to distribute service loads across the bond area and reduce concentrated peel or cleavage stress.
For example, a magnet positioned inside a supporting metal pocket may have better mechanical protection than a magnet attached to an exposed surface with no supporting features. The actual design must still account for the direction of centrifugal force, magnetic attraction, and other operating loads.
Mechanical Retention and Magnet Positioning
Adhesive bonding does not always need to provide the only means of retention.
Depending on the application, engineers may consider:
- Recesses or pockets that locate the magnet
- Shoulders or retaining features that limit movement
- Fixtures that hold the magnet during curing
- Mechanical capture combined with adhesive bonding
- Defined assembly sequences for multiple magnets
These features can reduce movement during assembly and provide additional protection against unexpected loading.
In rotating components, the retention design must be evaluated for operating speed, magnet mass, rotor geometry, temperature, and the worst-case loading conditions. Do not rely on a generic adhesive strength value to establish rotor safety.
Consider Temperature, Vibration, and Operating Environment
The adhesive must remain suitable throughout the assembly’s service life, not just during initial installation.
Temperature: Check both the minimum and maximum service temperatures, as well as short-term temperature peaks. The adhesive’s cured performance, the magnet’s temperature rating, and the metal substrate’s thermal expansion should all be considered.
Thermal cycling: Repeated heating and cooling can create stress at the interface because the magnet, adhesive, and metal substrate may expand and contract at different rates.
Vibration and impact: Dynamic loading can cause fatigue or progressive damage, especially when the joint contains edge defects or experiences peel stress.
Moisture and chemicals: Humidity, condensation, oils, coolants, cleaning agents, and other chemicals may affect the adhesive or the magnet coating. Compatibility should be verified under realistic exposure conditions.
For demanding applications, qualification may include thermal cycling, humidity aging, vibration testing, impact testing, and mechanical retention tests. The test plan should reflect the actual operating environment and applicable product requirements.
Magnet Bonding Assembly Process and Quality Control
A repeatable assembly process helps reduce variation between individual components and production batches.
A typical magnet assembly bonding workflow includes:
- Confirm the magnet drawing, material, coating, dimensions, and magnetization direction.
- Verify the metal substrate material and bonding-surface condition.
- Confirm the approved adhesive product, shelf life, storage conditions, and preparation requirements.
- Clean and prepare both bonding surfaces.
- Dispense the specified adhesive quantity and control the bondline.
- Position the magnet using a suitable fixture or locating feature.
- Maintain the required pressure and alignment during the fixture period.
- Complete curing according to the adhesive manufacturer’s instructions.
- Inspect the finished assembly and perform the defined retention or qualification tests.
For production applications, process controls should include adhesive batch traceability, mixing or dispensing control, curing records, fixture condition, and inspection criteria.
Testing should use representative production materials and geometry. A simple test on two flat metal coupons may not accurately predict the performance of a magnet bonded to a curved rotor or a coated housing.
Common Magnet Bonding Failures and How to Prevent Them
| Common failure | Possible cause | Prevention |
|---|---|---|
| Magnet detachment | Poor surface preparation or incompatible adhesive | Verify surface compatibility and preparation |
| Adhesive separation from magnet | Weak or damaged magnet coating | Confirm coating integrity and qualify the interface |
| Edge lifting | Excessive peel stress or poor joint geometry | Reduce peel loading and improve mechanical support |
| Incomplete bonding | Incorrect adhesive quantity or uneven bondline | Control dispensing and joint gap |
| Failure after heating | Adhesive or magnet temperature limits exceeded | Validate the complete assembly at operating temperatures |
| Failure under vibration | Fatigue, impact, or insufficient retention | Use suitable adhesive toughness and mechanical support |
| Magnet position shift | Inadequate fixturing during cure | Use locating features and controlled curing fixtures |
When a joint fails, inspect the fracture surfaces before changing the adhesive. Failure at the adhesive-to-magnet interface, within the coating, inside the adhesive, or at the metal substrate can indicate different underlying problems.
Conclusion
Reliable magnet bonding adhesive selection requires more than choosing a product with a high advertised strength. The magnet coating, metal substrate, surface preparation, bondline thickness, joint geometry, operating loads, and environmental conditions must be evaluated together.
Epoxy and structural acrylic adhesives are common starting points for industrial magnet bonding, while cyanoacrylate and flexible adhesive systems may suit more specific applications. The final choice should always be based on the actual materials, the adhesive manufacturer’s technical data, and validation of the complete assembly.
For custom magnetic assemblies, discussing the magnet material, coating, metal substrate, loading conditions, and production process early in the design stage can help reduce bonding risks and improve assembly reliability.
FAQs
What is the best adhesive for bonding magnets to metal?
There is no single best adhesive for every application. Two-part epoxy and structural acrylic adhesives are common options for industrial magnet bonding. The correct choice depends on the magnet coating, metal substrate, joint gap, service temperature, mechanical loading, and production requirements.
How do you glue neodymium magnets to metal?
First identify the magnet’s surface coating and the metal substrate. Clean and prepare both surfaces using an approved method, apply a compatible adhesive, control the bondline, position the magnet securely, and allow the adhesive to cure according to its technical instructions. Validate the finished joint under representative service conditions.
Is epoxy or acrylic better for magnet bonding?
Epoxy is often considered for structural joints requiring strong adhesion and environmental resistance. Structural acrylic may be preferable when faster fixture times and production efficiency are important. Neither is universally better; the specific formulation and assembly conditions determine performance.
Can magnets be bonded to painted or coated metal?
Yes, some adhesive systems can bond to painted or coated metal, but the coating itself becomes part of the joint. Its adhesion to the underlying metal and compatibility with the adhesive must be verified. A weak or poorly attached paint layer can cause the entire joint to fail.
How can magnet detachment be prevented in industrial assemblies?
Use compatible adhesive and surface preparation, control bondline thickness, design the joint to reduce peel and cleavage stress, provide accurate positioning during curing, and consider mechanical retention where appropriate. Qualification testing should reflect actual temperature, vibration, and loading conditions.